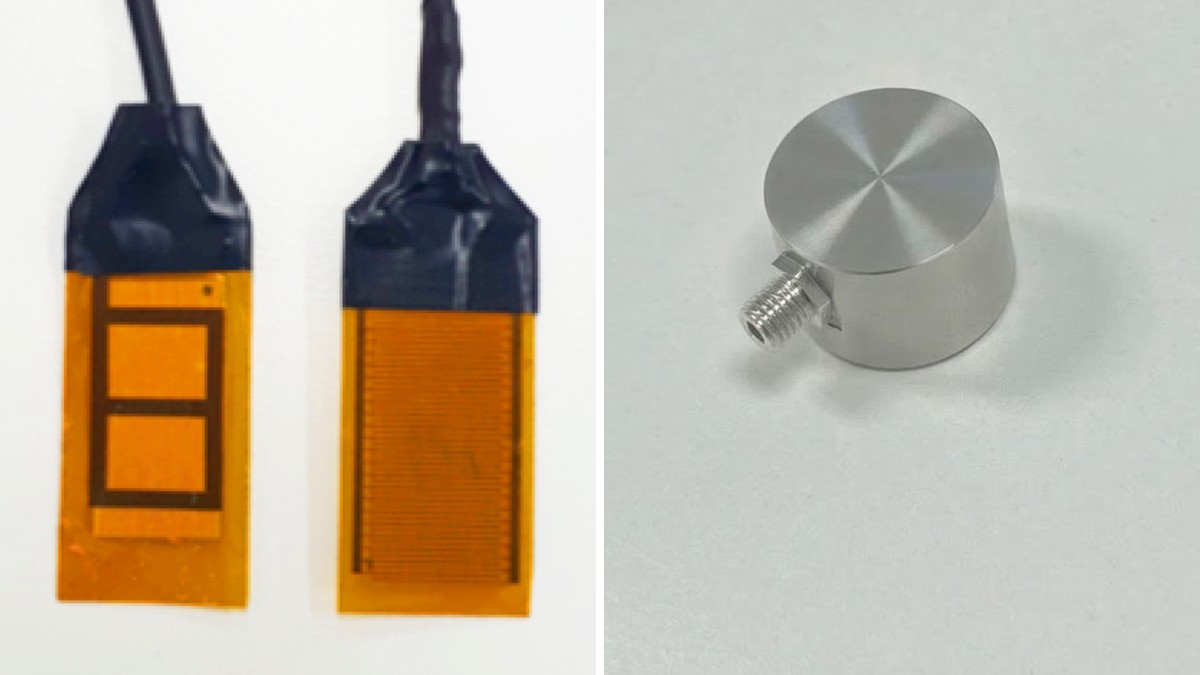
- Predictive maintenance (PdM) continuously measures equipment condition, finds early signs of failure, and schedules repair before the equipment breaks down.
- Unlike reactive maintenance (fix after failure) or preventive maintenance (replace on a schedule), it acts when maintenance is actually needed.
- Adoption starts with a few critical machines and on-site measurements to build a normal baseline.
When equipment stops, lost production often costs more than the repair itself. Yet replacing parts on a fixed schedule means throwing away parts that still have useful life. Predictive maintenance sits between the two: it decides when to service equipment based on the signals the equipment actually gives off. This article covers how maintenance strategies differ, how predictive maintenance works, and how to introduce it.
How do maintenance strategies differ?
Equipment maintenance falls into four broad approaches. The main difference is when maintenance happens.
| Strategy | When | Strengths | Limits |
|---|---|---|---|
| Reactive | After a failure | Little planning or overhead | Unplanned downtime, secondary damage to nearby parts |
| Preventive | On a fixed interval | Fewer sudden failures | Healthy parts get replaced; failures between intervals are missed |
| Condition-based (CBM) | When a reading crosses a limit | Driven by actual condition | Limits are hard to set; alarms can come late |
| Predictive (PdM) | Before an expected failure | Work and parts can be prepared in advance | Needs accumulated data and an analysis process |
The U.S. Department of Energy’s Federal Energy Management Program (FEMP) O&M guide reports that predictive maintenance can save roughly 8–12% compared with preventive maintenance and roughly 30–40% compared with reactive maintenance. Actual results vary with equipment type and operating practice, so it is worth validating on the target equipment first.
How does predictive maintenance work?
Predictive maintenance is a repeating loop, not a one-off measurement. Sensors collect condition data, meaningful features are extracted and compared with normal behavior, and confirmed anomalies feed into the maintenance plan. The results of each repair are then used to refine the decision criteria.
The normal baseline is the key
Even identical machines produce different signal levels depending on load, installation, and operating pattern. Rather than applying a generic limit, learning each machine’s normal signal first and tracking how far it drifts from that baseline helps reduce false alarms. The indicators used for these decisions are explained in AE signal parameters.
When do signs of failure appear?
Most equipment damage does not appear suddenly. Invisible changes such as micro-cracks or friction come first, and over time they lead to higher vibration, rising temperature, and noise. This progression is described by the P-F curve, which runs from the point where damage begins (P) to functional failure (F). The earlier the warning, the longer the P-F interval, leaving more time to source parts and schedule work.
AE (acoustic emission) sensors detect high-frequency elastic waves generated inside the material by crack growth or friction from poor lubrication, which makes them well suited to catching changes before vibration rises. The curve in AE sensor vs vibration sensor shows where each sensor picks up a fault.
Which equipment should come first?
There is no need to cover every machine at once. It is common to start with equipment that meets one of these conditions.
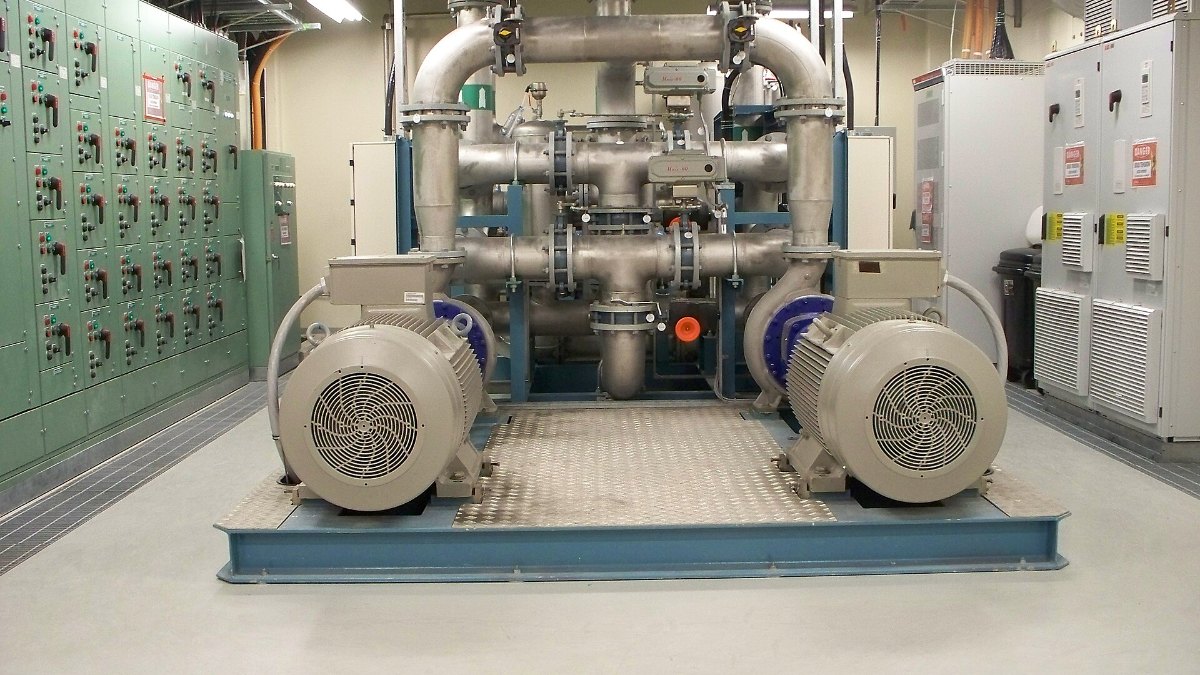
Pumps, compressors and main drive motors that stop the whole line when they stop
Machines with a history of bearing, gear or seal failures in the same place
Elevated or confined areas, pipes and tanks that cannot easily be stopped
High-pressure piping and hazardous storage where a leak can cause an accident
Which sensors are used?
| Sensor | Measures | Typical faults |
|---|---|---|
| AE sensor | High-frequency elastic waves inside the material | Early cracks, friction and lubrication problems, leaks |
| Vibration sensor | Amplitude and frequency of machine vibration | Imbalance, misalignment, advanced bearing damage |
| Temperature sensor | Surface or internal temperature | Overload, lack of lubrication, electrical faults |
| Current sensor | Motor current waveform | Load changes, electrical defects |
No single sensor covers every failure. Decide which failure modes you want to detect first, then choose the sensors that match. See the AE sensor selection guide for selection criteria.
How is it introduced?
Prioritize equipment by downtime cost and failure history.
Measure signals under real operating conditions to confirm detectability.
Fix sensor positions and signal paths for continuous measurement.
Accumulate normal operating data and set decision criteria.
Link alerts to maintenance planning and refine criteria from results.
Rather than rolling out plant-wide from day one, verifying on a few machines that normal and abnormal signals can be told apart, then expanding, keeps the cost of failure low. In noisy environments, also see How to Separate Real AE Signals from Field Noise.
AE-based predictive maintenance by RINA SOLUTION
RINA SOLUTION combines FlexMate, a flexible AE sensor that conforms even to curved pipes, the real-time monitoring platform FlexReal, and AI diagnostics FlexAI to cover everything from data collection to anomaly detection and alerts. We first confirm through on-site testing that normal and abnormal signals can be separated, then move to continuous monitoring. Real applications are shown on the use case pages below.
- What Is an AE Sensor (Acoustic Emission Sensor)? Principle, Applications and Selection
- How AE Detects Motor, Gear and Bearing Faults: Condition Monitoring for Rotating Machinery
- How AE Detects Pipeline Leaks: From Signal Characteristics to Leak Location
- How AE Detects Cracks and Damage in Equipment: From Crack Growth to Corrosion and Wear
Considering predictive maintenance?
Tell us about your equipment and operating conditions, and we will review everything from on-site measurement to the right scope.
Contact usGet the company profile